How to prepare a 3D model for printing: a checklist before you send the file

A model that looks perfect on screen can still fail on the printer. The screen forgives holes in the mesh, walls with zero thickness and parts floating in the air. The printer does not. Most problems in incoming files come down to the same seven things, and all of them are quicker to fix before printing than after.
1. File format
We accept STL, OBJ, 3MF and native CAD files. STL is the old standard and opens everywhere, but it stores only the surface: no units, no colour, no information about separate parts. 3MF keeps all of that in one file. If your software offers both, send 3MF.
If you work in CAD, send the native file or STEP as well. It is much easier to change a wall thickness in CAD than in a mesh.
2. A closed mesh
The model has to be watertight: one closed surface with no holes, no faces turned inside out and no stray geometry inside. Imagine filling it with water. If it would leak, the software that prepares the print cannot tell inside from outside.
Most modelling programs have a check for this, and the repair tools built into print preparation software fix simple cases on their own.
3. Wall thickness
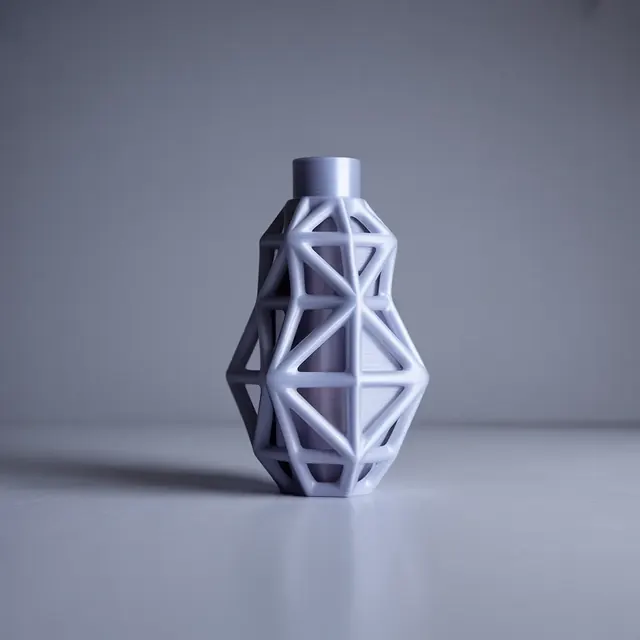
A wall thinner than the printer can build either disappears or breaks when the supports come off. As a starting point: about 1.2 mm for FDM, about 1 mm for SLS, and 0.6 to 1 mm for SLA depending on how tall the wall is. Large pieces need more.
These are rules of thumb. The real minimum depends on the material and the shape, and we check it before printing.
4. Scale and units
STL has no units. A model drawn in inches and opened as millimetres comes out 25.4 times smaller. A chair the size of a matchbox is a classic.
Write the overall dimensions in the message when you send the file: height, width, depth. It takes ten seconds and removes the guesswork.
5. Export resolution
Curves in a mesh are made of flat triangles. Export too coarse and a sphere prints as a faceted ball. Export too fine and the file grows to hundreds of megabytes with nothing to show for it. For most objects a deviation of 0.01 to 0.05 mm on export is enough.
A simple test: zoom in until the model on screen is the size it will be printed. If you can see the facets there, you will see them on the print.
6. Overhangs
Each layer needs something underneath it. Up to about 45 degrees from vertical a wall supports itself. Beyond that the printer adds supports, which are removed by hand and leave marks on the surface they touched.
You do not have to redesign the piece around this. But if there is a face that must be perfect, tell us which one, and the model will be positioned so the supports land somewhere else. SLS is the exception: the powder holds the part, so overhangs cost nothing. There is more on this in our comparison of the three technologies.
7. Parts that fit together
Two parts modelled to exactly the same size will not slide together. A lid needs clearance, a pin needs a slightly larger hole. For a fit that can be taken apart, 0.2 to 0.3 mm per side is a reasonable start, and more for large parts. When the fit is critical, a small test print of the joint settles it before the full job.
The same applies to big objects made of several pieces. How those joints are designed is covered in the article on printing in sections.
If there is no model yet
A sketch, a photo or a reference is enough to start a conversation. Our team handles CAD optimisation and file preparation, so tell us what you have.
What to write in the message
- what the piece is for and where it will stand;
- overall size;
- quantity;
- the finish you expect: raw, sanded or painted;
- the date you need it.
With that and a file we can quote without a long exchange of questions.