Architectural model making in Dubai: 3D printed scale models, detail and time
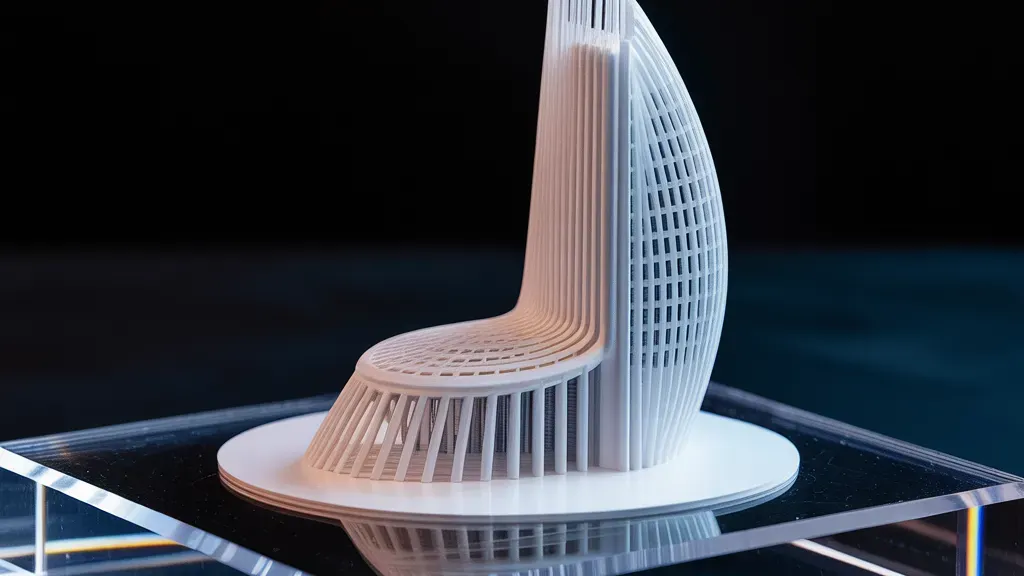
Scale is the first decision on an architectural scale model, and it decides almost everything after it. Pick 1:500 and a 200 m tower comes out 40 cm tall, which fits one print bed and reads as massing. Pick 1:100 and the same tower is 2 m tall, arrives in sections, and every balcony slab you drew now has to survive sanding and paint. The file does not change. The amount of work changes by an order of magnitude.
Most of the architectural models we print in Dubai fall into two jobs. One is an investor or client presentation where the model sits on a table in an air-conditioned room and has to hold up when someone leans over it from 40 cm away. The other is a stand model for a property show like Cityscape or a sales centre, where people walk past it, lean on the plinth, and a security guard moves it twice a day. Those two jobs want different scales, different materials and different finishes, even for the same building.
What follows is how we pick scale, what detail actually survives at each one, how we split models that are bigger than any printer, and what really drives the calendar — the questions worth putting to any model makers you approach here. No price list: every model gets quoted after we see the file, because two towers of the same height can differ threefold in print volume and part count.
Why architectural scale models still get ordered here
A render answers "what will it look like". A model answers "how does this sit next to the plot behind it" and, more often than anyone admits, "can four people stand around it and argue". We see the same three triggers.
Investor and board presentations, where a masterplan model with removable phase blocks does something a screen cannot: you lift phase two out and put it back.
Internal design review, usually a facade fragment at 1:50 or 1:20, printed to settle a disagreement about mullion rhythm or balcony depth that nobody can resolve in a 3D viewport.
Exhibition and sales use, where the model is a magnet for the stand and gets handled for a week straight. This is the one where material choice matters more than detail, because a beautiful 1:100 model in brittle resin does not survive four days of a trade show and a drive across town.
Choosing a scale: masterplan down to facade fragment
The useful way to choose is to convert one real dimension and see what you get. Floor-to-floor in a Dubai residential tower is usually around 3.2 m. Run that number through each scale.
1:1000 and 1:500, masterplan and district. At 1:500 a floor is 6.4 mm and a 1.2 m balcony is 2.4 mm. Individual balconies are gone. What you get is footprint, height relationship, road geometry, podium shape and landscape zoning. A 1.2 km by 800 m site comes out 2.4 m by 1.6 m, which is a tiled base, not a single print. This is the scale for phasing, approvals conversations inside the client's own team, and anything where the point is the whole plot.
1:200, the default for a single tower. A floor is 16 mm, a 200 mm slab edge is 1 mm, a balcony reads at 6 mm deep. A 120 m, 40-storey residential tower lands at 60 cm tall, which is a good table height. Facade rhythm is legible, window openings are legible, a 150 mm mullion is 0.75 mm and is at the edge of what we will print as a real feature rather than paint as a line. Most developer presentation models we make sit here.
1:100, when the facade is the subject. The same tower is now 1.2 m tall and comes in five or six stacked sections. A slab edge is 2 mm, a door is 9 mm, a 50 mm railing post is 0.5 mm, which is SLA territory and not FDM territory. Interior floor plates become possible, so cutaway models and a lifted-off roof start to make sense.
1:50 and 1:20, fragments. At 1:50 a floor is 64 mm, a door is 18 mm wide, a 40 mm handrail is 0.8 mm. At 1:20 a mullion is 7.5 mm and you are effectively printing a piece of the building. We get these as single bay fragments for material and detail sign-off, often with real glass substitute inserted rather than printed.
One rule from the bench: decide the scale before you decide the size of the table. People do it the other way round, land on a 2.2 m base for a stand that was going to hold a 1.5 m model, and then pay for the extra 40 percent of volume in material, in finishing hours and in crate size.
What detail survives at each scale
The physics is simple enough to plan around. On FDM we run a 0.4 mm nozzle for most model work, and layer heights typically between 0.1 and 0.3 mm. A wall thinner than about 0.8 mm is unreliable: it prints, then breaks off in sanding or in transit. Anything structural wants 1.6 mm or more. Tolerances on FDM are typically in the range of plus or minus 0.3 to 0.5 mm, which is fine for a tower section and useless for a 1:100 balustrade.
SLA is the other half of the answer. Layer heights of 0.025 to 0.1 mm, tolerances typically plus or minus 0.1 to 0.2 mm, and it will hold a 0.5 mm feature. That is where the railings, louvre fins, street furniture, fine tracery and any sculptural element on the facade get printed. The trade is toughness: standard resin parts are stiffer and more brittle, and they do not forgive being dropped.
So most serious architectural models here come out hybrid. FDM for shells, slabs, podium, terrain and the base, because the volume is large and nobody will ever see a 0.2 mm layer line under primer and paint. SLA for the small repeating parts that would otherwise look like a blob. Two technologies on one model, glued together after finishing. You can see how both behave on real parts in our materials and technologies section.
Two honest limits. Transparent glazing is the weakest point of printing: clear resin prints come out translucent rather than optically clear, and they yellow with time and UV. We usually read glass with paint value and surface sheen, or leave the opening for a cut sheet insert. And text, like a building name on a podium, stops being readable below roughly 2 mm cap height on FDM, so at 1:200 it is painted or applied, not printed.
Materials, and the Dubai variable
The climate question is not theoretical. The common FDM material, PLA, has a glass transition in the region of 55 to 60 degrees C. A closed car in an outdoor car park here in July goes past that, and a PLA tower comes back from a 20 minute drive with a lean in it. We have seen panels bow in a crate that sat on a loading dock in the afternoon.
For anything that travels, waits outdoors, or sits near glass in direct sun, we move to PETG, or ABS and ASA, where the softening range is considerably higher, and ASA holds up better under UV. Standard SLA parts stay dimensionally fine in the heat but get more brittle with prolonged UV, and uncoated resin yellows. Paint and primer help, because a pigmented coat is also a UV shield.
A model that lives permanently in an air-conditioned showroom is a much easier brief, and we will say so, because the right material there is whichever one finishes best, not whichever one is toughest.
From CAD file to assembled model
The path is the same every time, and the first step is where most of the delay hides.
File preparation. Architectural CAD is not print geometry. Walls arrive as single surfaces with no thickness, curtain walls arrive as hundreds of overlapping panels, and the terrain is usually an open mesh. We need closed, watertight solids, with every feature at or above the wall minimum for the chosen technology. Revit and Rhino exports also carry absurd part counts that have to be merged or thrown away. Our checklist for preparing a model for printing covers what to send and in what format, and sending the file that way typically removes days from the start of the job.
Sectioning. Anything bigger than a build volume gets split deliberately, along panel lines, floor slabs and setbacks, with registration keys or dowel holes so the parts land in one position and only one. Splitting on a horizontal plane through a feature line hides the seam. Splitting mid-facade does not, and no amount of filler fixes it later. We go deeper into this in the piece on large-scale printing in sections.
Printing. Multiple machines run in parallel, which is why a 2 m model is not twenty times the calendar of a 10 cm one. Print time scales with volume and layer height, not with how impressive the model looks.
Finishing. This is the part clients consistently underestimate. On FDM shells we typically go 180, then 320, then 400 grit, with filler primer between rounds, and a presentation model usually takes two or three primer and sanding cycles before paint goes on. Layer lines show up under paint like a tide mark if you skip one. SLA parts need washing, post-curing, support nub cleanup and a lighter sand.
Assembly and base. Sections bonded, joints filled and spot-primed, fine SLA parts fitted last so they do not get knocked off during handling, then the model goes onto its base with landscape, roads and labelling. If internal lighting is wanted, the cavities and cable routes have to exist in the file before we split anything.
Size, and where sectioning takes over
We print from 5 cm figures up to constructions reaching 15 m, and everything above a single build volume is printed in sections and assembled into one piece. For architectural work the practical thresholds are these: a tower up to roughly 40 cm can often be one or two prints, a 1 m tower is typically five or six stacked sections, and a masterplan base of 2 m or more is a tile grid on an internal frame with a rigid substrate underneath so it stays flat when four people lift it.
Shipping decides more than people expect. If the model has to fly, it gets designed to come apart into crate-sized modules on purpose, with hidden joints that can be opened and reclosed on site. Tell us that at the start, not after the base is bonded. Examples of assembled sectioned work are in the project gallery.
Lead times and what moves them
Typical working ranges, and they depend on the file and the finish level rather than on good intentions.
A single building at 1:500 or 1:200, unpainted or simply finished, is usually a matter of days once the file is clean. A painted presentation tower at 1:200 is commonly one to two weeks. A 1:100 sectioned tower, or a masterplan with multiple blocks, landscape and a finished base, typically runs two to four weeks, and more if the design is still moving while we print.
What actually moves the date, in order of how often it bites: file quality, because a week can disappear into repairing geometry that was never meant to be manufactured; finish level, because sanding and priming are hand hours and cannot be parallelised the way printing can; part count, because 200 small components means 200 cleanups and 200 glue-ups; and design changes mid-job, where a facade revision after printing means reprinting that section and refinishing it from bare plastic.
Fastest route to a model in hand, if the date is immovable: fix the scale early, accept a coarser finish on non-visible faces, keep the palette to two or three paint values, and freeze the geometry. A clean frozen file at a sensible scale beats a beautiful file that arrives in three versions.
What moves the number in a quote
We do not publish rates, because a model is quoted after we see the geometry. What we can tell you is what the estimate is built from: print volume in cubic centimetres, which drives material and machine time; number of discrete parts, which drives cleanup and assembly labour; technology mix, since SLA detail parts cost more per gram than FDM shells; finish level, from bare plastic to multi-coat painted presentation; base and landscape work; and urgency, which mostly buys machine priority and overtime on the hand work.
Send the file or even a massing sketch through the contact form or on WhatsApp and we will come back with a real number for your geometry.
Picking the scale for your own job
Short version. If the subject is the plot, go 1:500 or 1:1000 and spend the budget on base quality. If the subject is one building and the audience is investors across a table, 1:200 is the safe default. If the subject is the facade, go 1:100 and plan for sections, or print a 1:50 bay instead of the whole tower and get far more detail for less money. If the subject is a junction detail, 1:20 and treat it as a part, not a model.
And if it is going on a stand, tell us that first. It changes the material before it changes anything else.
FAQ
What is the real difference between a 1:200 and a 1:100 model?
Twice the height, roughly eight times the material volume, and a different category of work. At 1:200 a 120 m tower is 60 cm and often prints in one or two pieces, with facade rhythm legible and fine railings painted rather than printed. At 1:100 the same tower is 1.2 m, comes in five or six sections that have to be registered and seam-filled, and small features like 50 mm railing posts become 0.5 mm parts that need SLA. Choose 1:100 when someone has to read the facade, not when you want the model to look expensive.
How detailed can a printed architectural model actually be?
The limit depends on technology, not on ambition. On FDM, features below roughly 0.8 mm are not reliable, and tolerances are typically plus or minus 0.3 to 0.5 mm. On SLA we hold around 0.5 mm features with layer heights down to 0.025 mm and tolerances typically plus or minus 0.1 to 0.2 mm. In practice that means a 1:200 model shows openings, slab edges, balconies and setbacks cleanly, while cornices, louvres and balustrades need SLA parts or paint. Printed text stops reading below about 2 mm cap height on FDM.
How long does a 3D printed scale model take?
A simple single building at 1:200 or 1:500 is typically days after the file is clean. A painted presentation tower is commonly one to two weeks. A sectioned 1:100 tower or a masterplan with landscape and a finished base usually runs two to four weeks. The variables are file quality, finish level, part count and whether the design is still changing. We give a date against a specific file, not against a type of project.
Will a printed model survive Dubai heat and sun?
Indoors in air conditioning, yes, with almost any material. Outdoors, in a parked car, or next to a sun-facing window, PLA is the wrong choice, since it softens in the region of 55 to 60 degrees C and a hot car passes that. For those conditions we print in PETG, ABS or ASA, with ASA holding up best under UV, and we paint and prime, which also shields the surface. Uncoated resin parts yellow and get more brittle under prolonged UV, so for permanent outdoor display we discuss material and coating before anything goes on a printer.