3D printing packaging prototypes: bottles, jars and caps
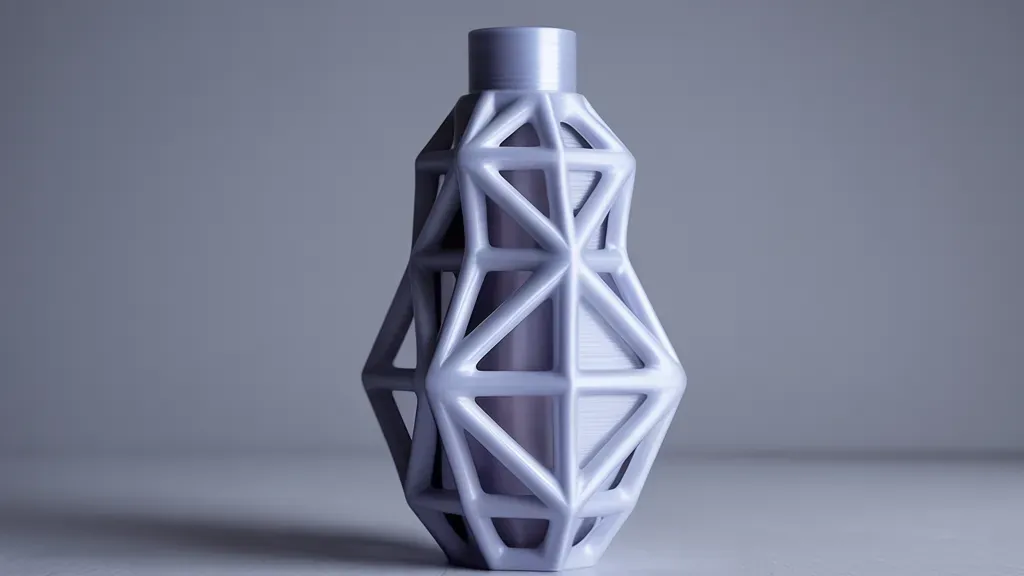
Packaging is the small, fussy end of what we print. A bottle is 180 mm tall and nothing about it forgives you: the thread has to accept a real cap, the wall has to read like the wall of the moulded part, and the weight in somebody's hand decides half the review. Next to a two-metre exhibition piece, a 60 mm closure is the harder job.
Most of what you find online about a 3D printing packaging prototype is written from the tooling side, and it argues about calendar time. Days against weeks, a printed part against a steel cavity. That argument is sound and it is not the thing that catches people out. What catches people out is that a printed thread binds half a turn in, that a printed bottle weighs roughly twice what the production one will, and that a wall thickness which prints beautifully cannot be injection moulded at all.
What the prototype is actually being asked to prove
Packaging prototypes arrive wanting one of a few different answers, and they are different prints.
- Proportion and silhouette. Does the 500 ml bottle look like 500 ml, does the shoulder radius read on a shelf, is the label panel big enough for the artwork.
- Fit. Does the cap engage, how many turns, does the flip-top click and stay closed, do the jars stack and nest.
- Hand feel. Grip width, where the thumb lands, whether a wet hand can open it.
- Capacity. The nominal volume against the real one.
The first of those wants a smooth painted shell and does not care about its own thread. The second wants a correct thread and does not care how it looks. Asking for both in one print usually gets you a compromised version of each, so we print the body and the closure as separate exercises more often than not.
FDM or SLA for a jar lid thread, and where each one lies to you
If you are still choosing between processes in general, FDM against SLA against SLS covers that ground. Packaging narrows it a lot, because a thread is the single most demanding feature in the whole category.
FDM lies to you about dimensions in a way that stacks. Internal features print slightly undersize, because the extruded line pushes a little inward around a curve. External features print slightly oversize for the same reason. A bottle neck is an external thread and a cap is an internal one, so both errors push the pair tighter. Two parts that each measured within a couple of tenths of the model will still refuse to screw together.
The second FDM problem is resolution across the thread profile. A 410 continuous thread on a 28 mm neck has a thread depth under a millimetre. At 0.2 mm layers that crest is described by three or four layers, so it comes off the plate as a staircase with a rounded top and a filled root. The cap catches, turns a third of the way, and stops.
SLA is the honest one here. Layers of 0.025 to 0.05 mm resolve the crest properly, the surface comes off slick enough to turn without sanding, and the flanks are geometrically where the file put them. Our rule on packaging is simple: the body can be FDM, the thread goes to resin.
What resin will not give you is torque. A standard resin thread strips under ordinary finger pressure, usually by shearing the flanks off at the root rather than cracking the wall. That is fine, as long as everyone understands what the part is proving. A resin closure tells you the geometry mates and how many turns to engagement. It does not tell you the cap survives a thousand openings, and nobody should ask it to.
Bottle cap design and 3D printing tolerance on the neck
Packaging has a vocabulary for this and using it saves whole rounds. A neck finish is described by four measurements, set out plainly on SKS Bottle's cap and neck finish reference: T across the outside of the thread, E across the neck outside the thread, S from the top of the finish down to the top edge of the first thread, and H for the height of the finish. T minus E, halved, is your thread depth. S is what decides how the closure lands and how much thread actually engages.
Call the finish out by its code, 28-410 or 24-400, instead of modelling a thread by eye. The code maps to a published specification with real tolerances, and it means a stock cap from a supplier can be tried on your printed neck on day one.
Numbers we work to, which describe our processes rather than promise anything about your geometry. FDM parts of this size typically land within two or three tenths of a millimetre, which on a thread under a millimetre deep is most of the feature. SLA on a part under 100 mm usually holds nearer a tenth. For a printed neck meeting a stock cap we start by offsetting the thread around 0.15 to 0.25 mm on FDM and roughly half that on resin, then correct on the next print. Nobody gets a thread right first time, and the fast way through is to print a 30 mm neck stub on its own rather than a whole bottle.
Orientation matters more than people expect. We print necks and caps with the thread axis vertical, so each layer is a closed ring and the thread spirals cleanly up it. Lay the same part on its side and you get support material inside the thread groove and an oval neck.
Wall thickness: what prints, and what survives injection moulding
This is where a packaging prototype before injection moulding most often misleads a team.
A blow-moulded PET bottle wall sits around a third of a millimetre. No printing process we run will build that, and it would not stand up if it did. Our practical floor on FDM with a 0.4 mm nozzle is about 0.8 mm, and anything that gets handled wants 1.2 mm or better. So a printed bottle body is three or four times thicker than the production part, stiffer, heavier and less translucent. We say this before printing, because a design review that concludes "it feels cheap" or "it feels solid" from a printed shell has concluded nothing.
Going the other direction is just as awkward. Protolabs' wall thickness guidance gives recommended ranges by resin, with ABS running roughly 1.1 to 3.6 mm, and asks that neighbouring features stay within 40 to 60 percent of the wall they join. A cap drawn with a 4 mm top and a 1 mm skirt prints perfectly and moulds badly, because the thick section cools last and pulls a sink mark into the face your artwork sits on.
Draft is the other thing printing hides. Printing needs none, so an unmouldable part looks finished on the bench. Protolabs recommends 0.5 degrees minimum on vertical faces with 1 to 2 degrees covering most cases, and more where a textured finish is involved. Add the draft to the model before the prototype round rather than after, so you see what a degree and a half does to a straight-sided jar. Sometimes it does nothing. Sometimes it changes the whole silhouette and the designer needs to know while there is still time.
Fit testing, seals and 3D printed food container prototypes
Fit testing is where printed packaging earns its keep, and most of it costs nothing but attention.
Count turns to engagement and mark the start angle, because a closure that lands with the pour spout pointing sideways is a real defect. Try the stock cap and the stock pump. Stack the jars and press down on the top one. Put a straight edge across the label panel. Check the gap between the cap skirt and the shoulder, since that is the line everyone sees on the shelf.
Leak testing needs a caveat. An FDM part seeps through its own walls along the layer bonds, so filling one with water tells you about the print, not about the seal. A resin part is monolithic once it is washed and cured, and it holds water, which makes a seal test on an SLA closure meaningful. We test with water, upside down, over a paper towel, for an hour. That finds a seal face that is out of flat. It does not qualify a liner or a gasket.
On food contact we are straight with people: a printed prototype is for fitting and measuring, not for filling. Layer crevices on FDM cannot be cleaned, and we are not going to certify a material we buy on a spool. The route teams take for food-safe samples goes through printed tooling instead of printed parts. Formlabs documents that approach in their write-up on how air up used printed rapid tooling to prototype food-safe bottles, where printed moulds fed silicone casting for the parts that touched a mouth. Their project, not ours, and a sensible pattern.
Capacity is the easy win nobody takes. Fill the printed container to the fill line, weigh the water, and you have the real volume in millilitres. We have handed back a 250 ml jar that held 232.
Clear resin when the production part is glass
Clear resin is the closest stand-in we have for glass, and it needs managing.
It does not come off the machine clear. The side that faced supports is cloudy, and the fine matte left by the process diffuses light. Getting to optical clarity means wet sanding up through progressively finer grits and then either a clear coat or a thin resin dip, the same finishing cycle we use on any print, except the gloss gets kept instead of killed. On a 200 mm bottle that is hours of hand work, and it is worth budgeting for rather than discovering.
Even finished, it will not feel like glass. Resin runs around 1.1 to 1.2 g/cm³ against roughly 2.5 for soda-lime glass, and our walls are thicker on top of that, so the mass is wrong in both directions at once. For a photograph or a shelf mock-up, clear resin is excellent. For a review about heft, hand somebody a weighted dummy instead.
Clear resin also yellows under ultraviolet. Left on a windowsill in Dubai it goes amber faster than anyone expects, so prototypes live in a box between meetings.
Predicting the weight of the moulded part
The slicer will tell you what the print weighs. That figure is nearly useless commercially, because it describes a thick-walled plastic stand-in.
What a moulder quotes on is grams of resin per part. Get it from the model instead: set the shell to the production wall thickness, read the solid volume off the CAD, and multiply by the resin density. Polypropylene is about 0.9 g/cm³, HDPE about 0.95, PET about 1.38. A 32 cm³ shell in PP is roughly 29 grams of material per part, and that number is worth arguing over before steel gets cut, because a gram on a closure multiplies by the whole run.
We run this calculation alongside the print on request. It takes minutes and it has changed more designs than any surface finish we have ever applied.
How many rounds it takes before tooling
On a closure, three or four rounds is normal. On a plain body, often two.
A round looks like this. The file gets checked and repaired, the parts get oriented and supported, the print runs overnight, then washing and curing for resin, support removal, measuring, fitting against stock components, and a written list of what moved. Small closure parts typically turn around in a day or two. A body that has to be sanded and painted takes longer, because primer dries on its own schedule. The general route from file to part is laid out in how a design file becomes a 3D printed prototype; packaging just runs it more times with tighter numbers.
The rounds tend to sort themselves the same way. The first one kills the obvious misses and the proportions. The second fixes the thread and the fit. The third deals with hand feel and whether the decoration survives the draft and the radii. The fourth exists because somebody changed the cap supplier.
Formlabs' own account of prototyping a multifunctional bottle with SLA describes the same escalation, with FDM used for the early shapes and resin brought in once the mechanical and cosmetic prototypes had to be accurate. That matches what we see. Early rounds do not need resolution. Late rounds need nothing else.
Hold your revisions until the part is on the table. Designers send updated files while the first print is still on the machine, and those edits are almost always reactions to a render. After an hour with the physical object the change list is shorter and cheaper.
Handing it to the moulder
The last printed round should be the geometry you intend to tool, draft and radii and all, not the pretty version from three rounds ago. Print it once more after those changes, because they alter the look.
Keep every round, labelled and dated, in a box. When a first-off part comes back from the tool and the argument starts about what was approved, the printed version with a date on the base ends it in thirty seconds.
Send a file, a sketch or a photograph of the container you want changed, along with the neck finish code if there is one, the production material and the date the tool has to be ordered. The form and the WhatsApp number are on the main page, and we quote each project after seeing what it involves.
FAQ
Can you 3D print a bottle cap thread that actually screws on?
Yes, and we do it most weeks, with SLA rather than FDM. Resin at 0.025 to 0.05 mm layers resolves a thread profile under a millimetre deep, and the part turns smoothly against a stock cap. Expect to tune the clearance once: we start around a tenth of a millimetre of offset on resin and correct after the first fit. What a printed thread will not do is take repeated torque, because the flanks shear at the root. It proves the geometry and the turns to engagement, not durability.
How many iterations does packaging usually need before injection moulding?
Typically three or four on a closure and around two on a bottle or jar body, though it depends heavily on how settled the design was when it arrived. A closure round is normally a day or two from file to measured part. A body that needs sanding and paint takes longer, since filler and primer set on their own schedule. The rounds get cheaper as they go, because the file preparation and support planning carry over and only the changed geometry needs new thinking.
FDM or SLA for a jar lid thread, and what breaks first?
SLA for the thread, every time. FDM prints internal features undersize and external ones oversize, so a printed neck and a printed lid both drift tighter and bind, and 0.2 mm layers turn a shallow thread crest into a staircase. FDM is the right choice for the body, where a hollow shell with internal ribs takes handling well. What breaks first on a resin lid is the thread flank under finger torque; what breaks first on an FDM lid is nothing, because it never screwed on.
What is the minimum wall thickness for a printed packaging prototype?
On FDM with a 0.4 mm nozzle, about 0.8 mm will print and 1.2 mm survives being handled. SLA goes thinner on small parts. The catch is that production packaging is often thinner than either: a blow-moulded PET bottle wall runs around a third of a millimetre. So the printed shell is stiffer and heavier than the real thing and should not be used to judge how the container feels. Going the other way, Protolabs publishes recommended moulding ranges by resin with ABS at roughly 1.1 to 3.6 mm and neighbouring features held within 40 to 60 percent of the wall they meet, which is worth checking before a thick cap top gets approved.
How do I check whether a cap seals on a printed prototype?
Use a resin part, not an FDM one. FDM seeps through its own layer bonds, so water escaping tells you about the print rather than the closure. On a washed and cured SLA part, fill it, close it, invert it over a paper towel and leave it an hour. That catches a seal face that is out of flat or a thread that bottoms out before the cap lands. It does not validate a liner, a gasket or long-term containment, and no printed part should be filled with anything anyone intends to eat or drink.
Will a clear resin bottle look like glass?
In a photograph, convincingly. In the hand, no. Clear resin arrives cloudy on the support side and needs wet sanding through fine grits plus a clear coat or resin dip to reach optical clarity, which is hours of hand finishing on a bottle-sized part. Even then resin is around 1.1 to 1.2 g/cm³ against roughly 2.5 for soda-lime glass, and our walls are thicker, so the weight is wrong. It also yellows under ultraviolet, so a clear prototype belongs in a box rather than on a windowsill.